 FRAMSTEG
Zinc Ingot Zn99.995: Kvalitet, Bundle Weight and Galvanizing Bath Use
Zinc Ingot Zn99.995: Kvalitet, Bundle Weight and Galvanizing Bath Use
Zinc ingot is the raw material behind almost every corrosion-resistant steel surface in the built environment. When a steel fabricator says a guardrail, a transmission tower or a scaffold board is galvanized, the coating that protects it began life as a stack of silver-grey blocks in a smelter yard. Those blocks are graded, weighed, marked and shipped with a chemistry that determines whether the coating will be uniform, whether the bath will behave predictably, and whether a die caster will get the mechanical properties it promised.
This guide examines the highest commercial grade in common circulation, Zn99.995, together with its neighbours in the standard. It explains what the four-digit purity actually controls, how a bundle of 48 ingots is built and reconciled, how the metal behaves in a galvanizing kettle or a die-casting machine, and where buyers most often lose money: on grade substitution that looks harmless on the purchase order and turns into a complaint six months later at a construction site.
1. What Zinc Ingot Is and Where It Is Consumed
A zinc ingot is a cast block of refined zinc, produced either by electrolytic refining of zinc sulphate solution or by thermal distillation and refining, then cast into a standard tapered mould and stacked into bundles. It is not alloyed, and apart from a small aluminium addition made for specific coating applications, it is sold as a near-pure metal whose value is set by the London Metal Exchange plus a regional premium and a grade adjustment.
The largest single consumer is the steel coating industry. Continuously galvanized sheet lines melt zinc and add aluminium to form a bath that produces the thin, formable coatings used in automotive bodies, appliances and roofing. Batch hot-dip galvanizing plants melt zinc in ceramic kettles at around 445 till 460 degrees Celsius and dip fabricated steel into it, producing the thick, sacrificial coating seen on highway furniture, transmission towers and structural steel. Both processes consume ingot by the tonne and both are sensitive to the same impurity families: leda, cadmium, tin, iron and aluminium.
The second large consumer is die casting. The Zamak family, covering alloys 3, 5 och 2, is made by melting high-grade zinc with aluminium, magnesium and copper. The rule that governs this application is simple and unforgiving: the base zinc must be cleaner than the alloy specification requires, because there is no refining step inside a die-casting shop. Impurities that enter with the ingot stay in the casting, and they express themselves as intergranular corrosion, dimensional instability or poor surface finish.
Other consumers are smaller but numerous. Brass mills add zinc to copper to make CuZn alloys. Rolled zinc strip plants produce sheet for roofing, battery cans and architectural panels. Oxide and dust producers feed zinc into chemical processes. Sacrificial anodes for hulls and pipelines are cast from a controlled zinc alloy. In every case the ingot is a charge material, and its commercial form, 25 kg tapered blocks stacked in bundles, is designed for charging cranes, forklift forks and furnace buckets.
2. Grade Designation and Chemical Composition
Chinese zinc ingot grades are defined by GB/T 470, in its current edition. The number after “Zn” is the minimum zinc content, and the remaining allowance is divided among lead, cadmium, iron, copper, tin, aluminium and other residuals. The difference between 99.995 och 99.99 percent sounds like rounding. In practice it is the difference between a metal that a die caster can use for automotive castings and one that belongs in a galvanizing kettle where a few parts per thousand of lead are tolerable.
| Kvalitet | Zn min (%) | Pb max (%) | Cd max (%) | Fe max (%) | Sn max (%) | Typical application |
|---|---|---|---|---|---|---|
| Zn99.995 | 99.995 | 0.003 | 0.002 | 0.001 | 0.001 | Die casting alloys, battery zinc, high-purity chemical use |
| Zn99.99 | 99.99 | 0.005 | 0.003 | 0.002 | 0.001 | Continuous galvanizing, brass making, rolled strip |
| Zn99.95 | 99.95 | 0.020 | 0.005 | 0.005 | 0.002 | Batch hot-dip galvanizing, general coating work |
| Zn99.5 | 99.5 | 0.30 | 0.02 | 0.02 | 0.01 | Prime Western type, heavy galvanizing, anode stock |
Two impurities deserve separate discussion because they cause problems that cannot be corrected downstream.
Lead. Lead is soluble in liquid zinc but only slightly soluble in solid zinc. During solidification it segregates to grain boundaries. In a galvanized coating this is tolerable at the levels permitted by the coating grades, and in fact small lead additions historically improved coating drainage and appearance. In a die casting, however, lead at the hundredths-of-a-percent level promotes intergranular corrosion: the casting swells, cracks and loses dimensional stability months after delivery. This is why Zamak specifications cap lead at 0.003 till 0.004 procent, and why the base metal must be Zn99.995 rather than Zn99.95.
Cadmium and tin. Both are harmful in die casting for the same reason as lead, and both are restricted in coatings intended for food contact or drinking water. Tin also interferes with the aluminium-rich intermetallic layer in continuous galvanizing when present above trace levels, producing bare spots and poor adhesion.
Iron is different again. Iron in the zinc bath is inevitable, because the steel being coated dissolves into the bath. Control is by periodic removal of dross, known as hard zinc, rather than by purchasing cleaner ingot. A buyer who pays for Zn99.995 to solve an iron problem in a galvanizing kettle has spent money on the wrong variable.
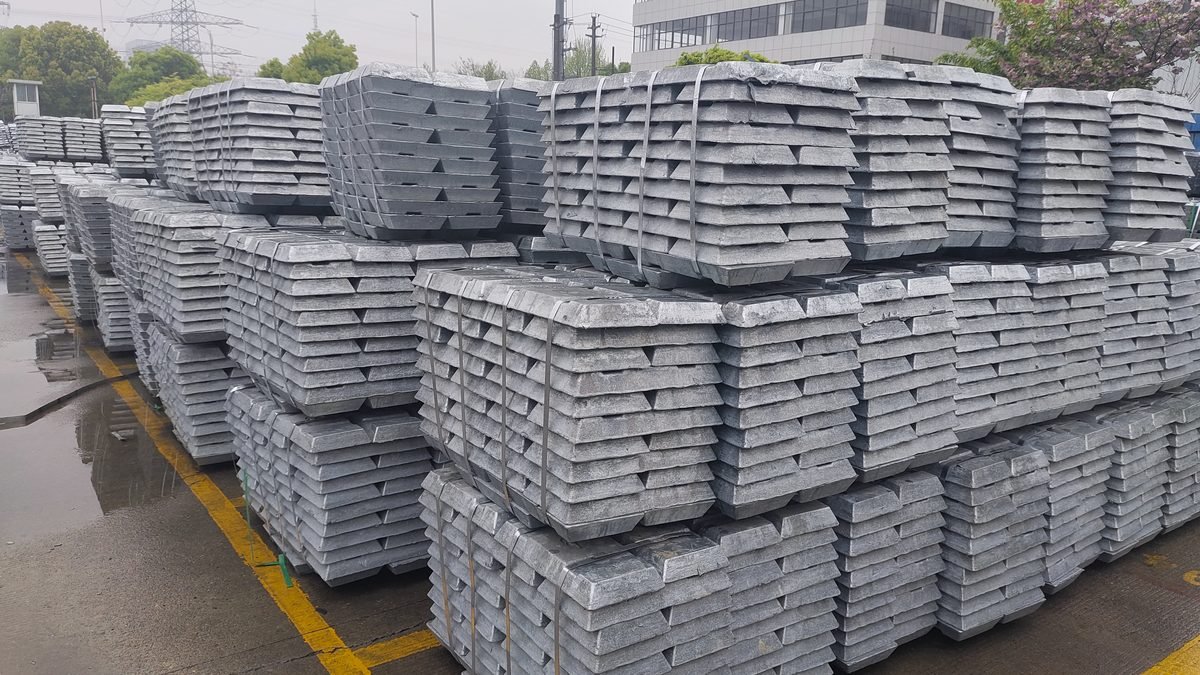
3. Physical and Thermal Properties
Zinc is dense, low-melting and comparatively soft, and each of those properties shapes how the metal is handled, melted and used. The numbers below apply to high-grade zinc at room temperature.
| Egendom | Värde | Why it matters in practice |
|---|---|---|
| Density at 20 °C | 7.14 g/cm³ | A 25 kg ingot is a compact block; a pallet of ingots is heavy for its volume and needs rated racking |
| Smältpunkt | 419.5 °C | Low enough to melt in a steel kettle; kettle life depends on tight temperature control, not on chemistry alone |
| Boiling point | om 907 °C | Fume generation rises sharply above 500 °C; extraction is a health requirement, not an option |
| Värmeledningsförmåga | om 116 W/m·K | Rapid heat transfer into steel, which is why the coating forms in seconds |
| Elektrisk ledningsförmåga | om 27 till 28 % IACS | Zinc is used as a conductor only in specialized battery and grounding work |
| Draghållfasthet, cast | om 110 till 150 MPa | Adequate for anodes and sacrificial components, far below structural requirements |
| Hårdhet | om 35 till 45 HB | Mjuk; ingots deform under sharp forks and can jam in a charging bucket if dropped |
| Crystal structure | Hexagonal close packed | Limited ductility at room temperature; rolled zinc strip needs warm rolling |
| Standard electrode potential | om -0.76 V | The entire logic of sacrificial protection: zinc corrodes so that steel does not |
The last line is the commercial reason zinc exists as a coating metal. Because zinc is less noble than iron, a zinc coating protects steel not only as a barrier but also as a sacrificial anode. A scratch that exposes bare steel will not rust immediately, because the surrounding zinc corrodes preferentially and keeps the steel cathodic. That protection is what pays for the galvanizing kettle, and it depends on a coating with the right thickness and the right composition, which in turn depends on a bath fed with the right ingot.
4. Ingot Weight, Bundle Data and Tolerances
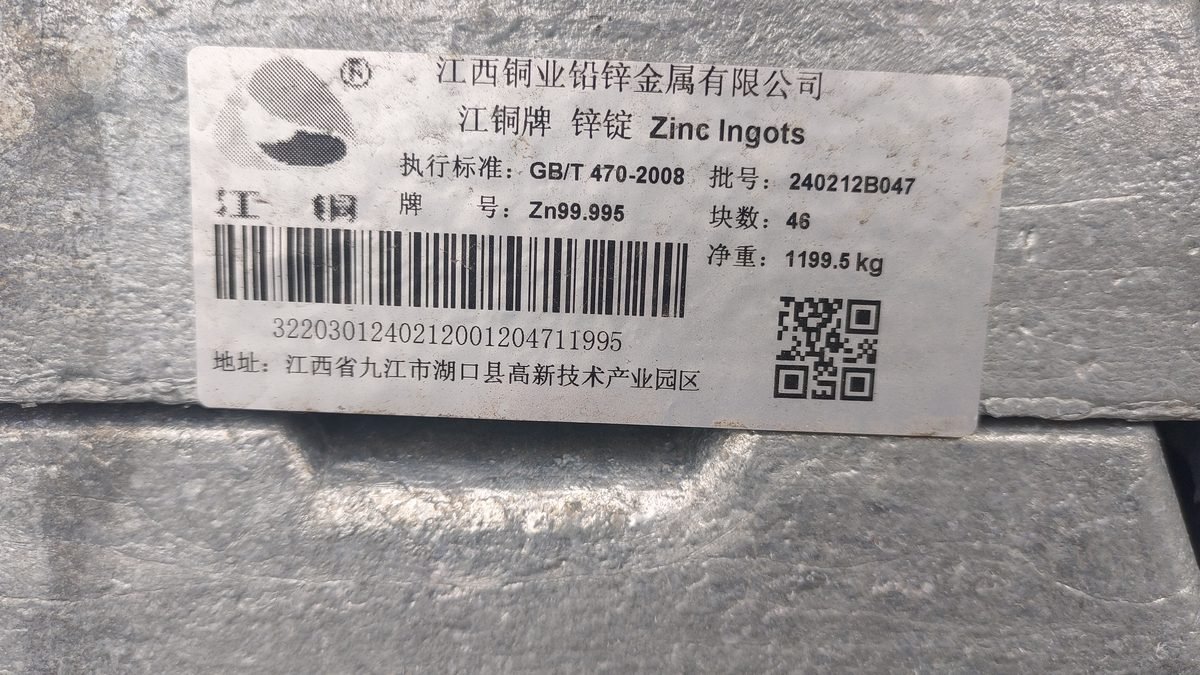
The standard commercial zinc ingot weighs 25 kg. A bundle is assembled from a fixed count, strapped, labelled and weighed as a unit. The label in the photograph below is a complete engineering document in miniature: it names the producer, the brand, the standard, the grade Zn99.995, the batch, the piece count of 48 and a net weight of 1199.5 kg. Divide the net weight by the count and you get 24.99 kg per piece, which is the correct way to verify that a bundle was built to specification rather than assembled from leftovers.
| Punkt | Typical value | Notera |
|---|---|---|
| Single ingot weight | 25 kg | Tolerance commonly plus or minus 1 kg per piece |
| Pieces per bundle | 46 till 48 | Marked on the label; even numbers simplify counting and stacking |
| Bundle net weight | om 1150 till 1200 kg | Weighbridge tolerance typically one percent |
| Ingot length | om 400 till 420 mm | Short enough for one person to handle and for furnace buckets |
| Ingot width | om 100 till 110 mm | Narrow so bundles stack compactly and metal melts evenly |
| Ingot thickness | om 55 till 65 mm | Tapered faces allow clean stripping from the mould |
| Bundle strapping | Steel or PET bands, 2 till 4 per bundle | Bands must not cut into the ingot surface deeply; a cut band is a handling hazard |
| Yta | Bright to dull grey | A white basic carbonate film is normal and harmless in remelting |
| Märkning | Cast-in brand plus paper label | Stämpla, kvalitet, sats, count, nettovikt, producer address |
Because zinc is priced on the London Metal Exchange, the difference between a 1199.5 kg bundle and a 1150 kg bundle is real money at scale. A shipment of 20 bundles that is short by 49 kg each is nearly a tonne of metal missing from the invoice. The reconciliation, count times unit weight against net weight, is the fastest defence and requires only a calculator.
5. How Zinc Ingot Is Produced
Nearly all high-grade zinc passes through one of two routes. The electrolytic route dominates modern production: zinc concentrate is roasted, leached with sulphuric acid, purified to remove copper, cadmium and cobalt, and then deposited as pure metal on cathodes in a cell house. The cathodes are stripped, melted in an induction furnace and cast into ingots. Because the purification step is chemical and the deposition step is electrochemical, the electrolytic route can reach 99.995 percent and can control lead and cadmium tightly.
The thermal route, still important in some regions, reduces roasted concentrate with coke in a retort or blast furnace, then refines the vapour by fractional distillation. Distillation separates zinc from lead and cadmium effectively, and the resulting metal is re-melted and cast. Both routes end in the same casting line: a chain conveyor with water-cooled moulds, a launder distributing metal, a stamping station and a bundling station.
Casting temperature for zinc is low, typiskt 450 till 480 degrees Celsius, and the metal is poured into cast iron or steel moulds. Because zinc contracts on freezing, the moulds are slightly tapered so the ingot releases cleanly. Surface appearance is a direct function of mould temperature and coating: a bright ingot indicates a clean, cool mould, while a dull, wrinkled surface points to a hot mould or a damaged release coating. Neither condition changes the chemistry, but both are useful indicators of housekeeping at the smelter.
Marking is part of the production line, not an afterthought. A cast-in brand identifies the producer permanently, while the paper or plastic label carries the batch and weight data that a certificate of analysis can be matched against. Losing that label is the equivalent of losing the certificate, because a bundle of grey blocks with no paper is indistinguishable from a bundle produced by anyone.
6. Selection Rules: Which Grade Belongs in Which Bath
The choice of grade is decided by the process, not by the price list. The rules below are the ones that experienced galvanizers and die casters apply without debate.
Continuous galvanizing lines. Use Zn99.99 or better. The bath is held at about 460 degrees Celsius with 0.15 till 0.25 percent aluminium, and the coating quality depends on a stable aluminium-zinc-iron intermetallic layer. Lead and tin disturb that layer. Iron is controlled by dross removal, not by ingot choice.
Batch hot-dip galvanizing. Zn99.95 is the working grade for most kettle operations, and Zn99.5 is acceptable where coating thickness rather than surface finish is the priority. Small lead contents help drainage and give a smoother, brighter coating; this is the one application where a slightly less pure metal is often preferred, and it is legitimate as long as the end product specification allows it.
Die casting. Zn99.995 is not optional. Zamak 3 and Zamak 5 both cap lead at 0.003 till 0.004 percent and cadmium at 0.002 till 0.003 procent. A base metal at Zn99.95 can carry five times that lead allowance, which is enough to trigger intergranular corrosion in service. When a casting fails on a machine tool after two years, the conversation always returns to the ingot certificate.
Brass and copper alloys. Zn99.99 is normally adequate. The copper alloy specification controls the final composition, and residual lead in the zinc is diluted by the copper charge.
Sacrificial anodes. Anode alloys are specified by their own standards and normally use Zn99.995 as the base, with controlled additions of aluminium and cadmium or indium. Using a lower grade introduces stray electrochemical behaviour that shows up as uneven consumption.
Chemical and battery uses. Zn99.995 minimum, and often a specific certificate for cadmium and lead is requested because both are regulated in batteries and in pigments.
7. Lagring, Handling and Safety
Zinc ingots are stable in storage. They do not rust, they do not degrade with rain and they can sit in an open yard for years without metallurgical loss. The white film that forms on damp surfaces is basic zinc carbonate, a thin passivating layer that disappears in the melt. This robustness is why yards are often open, as the photographs here show.
Handling is where the real risks sit. A 25 kg ingot is heavy enough to break a foot and compact enough to be dropped on one. Bundles at 1.2 tonnes must be lifted with rated slings under the bundle, never with the strapping. Forklift tines should enter the pallet, not the gaps between ingots, because a tine that lifts two ingots from the middle of a bundle will spill the rest.
Melting carries two specific hazards. The first is moisture. Water trapped between ingots, or ice in a winter yard, flashes to steam under molten zinc and throws metal. Ingots must be dry and above ambient dew point before charging. The second is metal fume fever. Zinc vapour produced above 500 degrees Celsius causes a flu-like illness in exposed workers. Local exhaust ventilation, respiratory protection during kettle charging, and strict temperature control are the controls, in that order.
There is also a documented interaction between zinc vapour and certain cleaning agents, and a well-known hazard when galvanized steel is welded or cut without extraction. Neither belongs to the ingot itself, but both belong to the process the ingot feeds, and a buyer specifying galvanized steel should assume the fabricator knows them.
8. Common Mistakes
Buying Zn99.95 for die casting. The most expensive mistake in this product family, because the failure appears months after the castings have been machined, painted and shipped.
Buying premium grade to fix a bath problem. Järn, aluminium drift and dross in a galvanizing kettle are process problems. Upgrading the ingot does not remove them and adds cost to every tonne.
Accepting bundle weights without reconciliation. Net weight divided by piece count should equal unit weight. If it does not, the bundle was not built to the label.
Treating the white surface film as corrosion. It is not. Rejecting a load for a harmless carbonate film is a costly misunderstanding of how zinc behaves in air.
Cutting strapping to count ingots. Open bundles in a yard lose their identity and their weight verification. Count the label, weigh a sample, keep the bundle intact.
Charging wet or icy ingots. A steam explosion in a kettle is not a theoretical risk; it is the most common serious accident in batch galvanizing plants.
Storing ingots on the ground without bearers. Water sits under the stack, the bottom ingots corrode into the concrete and the whole bundle becomes a handling problem.
Mixing grades in one kettle without records. Once two grades are in the bath there is no way to unwind the chemistry, and the coating specification is no longer demonstrable.
9. Vanliga frågor
What does Zn99.995 mean exactly? At least 99.995 percent zinc by mass, with lead at or below 0.003 procent, cadmium at or below 0.002 percent and the other specified residuals at trace level. The certificate of analysis gives the actual figures for the batch.
Can I use the same ingot for galvanizing and die casting? Technically yes for Zn99.995, but there is no commercial reason to pay for die-casting purity in a kettle that tolerates lead. Use the grade the process needs.
Why is zinc priced differently from aluminium? Zinc trades on the London Metal Exchange with a published cash settlement, so ingot prices move with the LME plus a regional premium. Aluminium follows its own LME contract and its own premium structure.
Does the bundle label matter after delivery? It matters more after delivery than before. It is the only link between a coating failure or a casting complaint and the heat that caused it.
How much does a bundle weigh? Om 1.15 till 1.25 tonnes net for 46 till 48 pieces at 25 kg each. Gross weight adds pallets and strapping.
Is there a difference between electrolytic and distilled zinc? In final purity, both routes can meet the same grade. In trace element pattern, electrolytic metal typically shows very low lead and cadmium, which suits die casting and battery work.
Can galvanized scrap be remelted into ingot? Ja, through a secondary smelter, but the coating introduces aluminium and the steel introduces iron. Secondary zinc is sold to its own specifications and is not interchangeable with primary Zn99.995.
What is the shelf life of an ingot? There is none in a metallurgical sense. Handling damage and label loss are the practical limits, not oxidation.
Why do some galvanizers ask for lead-free zinc? Because their end customer requires it, usually for drinking water contact, food equipment or a specific coating standard. The request is a product specification, not a preference.
What should I do if the certificate does not match the label? Stop the shipment, quarantine the bundles, and ask the supplier to re-issue a certificate referencing the batch numbers on the labels. Do not melt the metal until the discrepancy is resolved.
Sourcing zinc ingot or galvanized steel?
We can quote Zn99.995 and Zn99.95 ingots, hot-dip galvanized tube, strip and structural sections with grade certificates and bundle-level weights. Tell us the grade, tonnage and destination, and we will confirm the commercial terms.
Related reading: DX51D galvanized steel strip · varmförzinkat runt rör · C11000 kopparplåt

