 PROGRESUL
Bobina din oțel inoxidabil 304: Greutatea bobinei, Inner Diameter and Container Loading
O 304 stainless steel coil is a continuous length of cold rolled or hot rolled strip, wound into a single pack for transport and downstream processing. It is the raw material behind most 304 sheet that reaches a service centre, a kitchen equipment factory, a lift panel workshop or a chemical plant. Purchasing a coil looks simpler than purchasing a sheet, because there is only one line item on the enquiry, yet the parameters that decide whether the coil works on the buyer’s line are not thickness and grade alone. Greutatea bobinei, diametrul interior, outer diameter, edge condition and winding tension decide whether the coil can be lifted, decoiled, slit and levelled without scrap.
This guide covers 304 coil as a product: what it is, which chemistry and mechanical values the standard actually guarantees, how dimensional tolerances are written, how coil geometry translates into container payload, and which handling rules prevent edge damage and surface marking before the strip reaches the press.
1. What a 304 Stainless Steel Coil Is and Where It Is Used
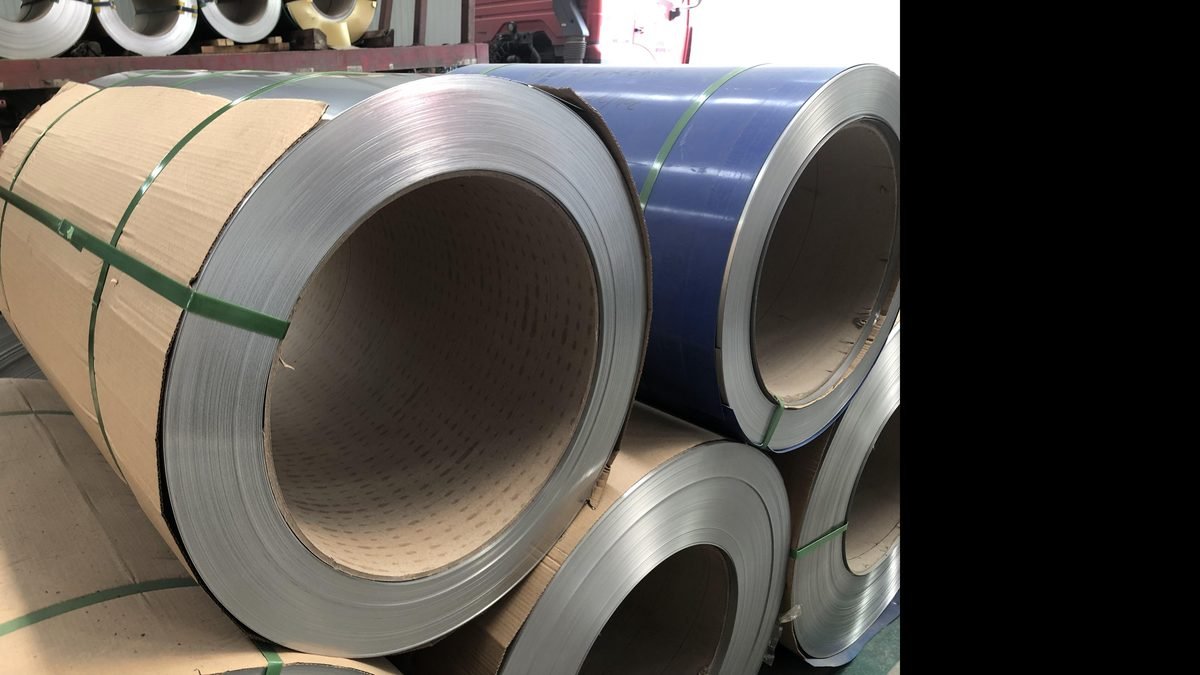
A coil is strip metal wound around a hollow core. The strip itself is produced either by hot rolling a slab and annealing and pickling the result, or by cold rolling an annealed hot rolled coil down to final thickness, followed by annealing and a finishing pass such as 2B, BA or No.4. The coil is then slit to the ordered width, edge trimmed, interleaved with protective paper or film where required, and banded for shipment.
In trade terms, o 304 coil is described by five values that appear on every mill certificate and packing list: nota, grosime, lăţime, coil weight and inner diameter. A sixth value, starea marginilor, is often left off the enquiry and then becomes the source of a claim.
Typical applications of 304 coil include:
- Cold rolled sheet and strip for kitchen equipment, chiuvete, counters and catering cabinets.
- Architectural cladding, lift car panels, column cladding and decorative trim.
- Slit narrow strip for roll forming of door frames, window sections and appliance trim.
- Tancuri, hoppers and process vessels in food, dairy and pharmaceutical service.
- Tube mills and welded pipe lines, where coil is the input strip.
- Stamped and deep drawn parts such as sink bowls, cookware shells and burner components.
- General fabrication where a corrosion resistant surface is required but 316L is not justified.
The same grade is sold as coil, foaie și farfurie. The difference is form and handling, not metallurgy. A buyer who needs 1.2 mm sheet in 1219 x 2438 mm blanks can buy cut sheets, but a buyer who runs a slitting line or a roll forming line buys coil because the continuous length is what the line consumes.
2. Grad și compoziție chimică
304 is the austenitic chromium nickel grade defined in ASTM A240, ÎN 10088-2, JIS G4304 and GB/T 4237. The chemistry that matters commercially is chromium for the passive layer, nickel for austenite stability, and carbon for strength versus weldability. The table below shows the standard composition limits, with 304L included because the low carbon variant is frequently supplied under the same commercial description.
| Element | 304 (%) | 304L (%) | Effect on the coil |
|---|---|---|---|
| C | 0.08 max | 0.030 max | Strength and hardness; lower carbon improves weld and heat affected zone |
| Si | 0.75 max | 0.75 max | Dezoxidarea; excess raises pickling difficulty |
| Mn | 2.00 max | 2.00 max | Austenite stabiliser, replaces part of the nickel |
| P | 0.045 max | 0.045 max | Segregation, cracking risk in welding |
| S | 0.030 max | 0.030 max | Machinability versus weld quality |
| Cr | 18.0 la 20.0 | 18.0 la 20.0 | Passive layer; the main corrosion reserve |
| În | 8.0 la 10.5 | 8.0 la 10.5 | Austenite stability, toughness, formabilitatea |
| N | 0.10 max | 0.10 max | Rezistenţă; too high reduces ductility |
Two commercial consequences follow from this table. Primul, a mill that works at the bottom of the nickel range produces a coil that is cheaper and perfectly legal, but with less austenite stability and a lower tolerance for heavy forming or warm service. Doilea, a coil ordered as 304 and delivered as 304L is not a substitution to be rejected automatically, because 304L meets the mechanical minimums for most sheet applications; it becomes a problem only where a customer specification or a pressure design explicitly calls for the higher carbon grade.
3. Proprietăți mecanice
Mechanical values for 304 coil are quoted in the annealed and pickled condition, which is the condition in which the coil is normally sold. A coil that has been slit and then cold worked will be stronger and less ductile in the worked zone, and that local difference is the reason a part sometimes cracks along a bend line even though the certificate says 40 percent elongation.
| Proprietate | Valoare tipică | Standard minimum | Sens practic |
|---|---|---|---|
| Tensile strength Rm | 620 la 700 MPa | 515 MPa | Design strength for non pressure parts |
| Yield strength Rp0.2 | 240 la 310 MPa | 205 MPa | Springback and forming load |
| Elongation A50 | 45 la 55 % | 40 % | Bend radius and deep drawing limits |
| Hardness HRB | 70 la 85 | 92 max | Shearing force and tool wear |
| Densitate | 7.93 g/cm3 | Reference value | Coil weight calculation |
| Elastic modulus | 193 GPa | Reference value | Deflection, springback, buckling |
| Dilatare termică | 17.3 x 10⁻⁶ /K | Reference value | Welding distortion, fit up gaps |
| Conductivitate termică | 15 la 16 W/mK | Reference value | Heat tint after welding, drying of wet coils |
The gap between typical and minimum values is the buyer’s real margin. A coil at the minimum 205 MPa yield and 40 percent elongation behaves noticeably differently from a coil at 280 MPa and 50 la sută, and the difference shows up in bend allowance and in the number of rejects at the press brake. When a job is sensitive to forming, it is worth asking for the actual test values from the heat number rather than accepting the standard minimums as a promise.
4. Dimensiuni și toleranțe
Coil dimensions are written as thickness, lăţime, inner diameter and weight. Tolerances are usually quoted against a table rather than a single number, because the permitted deviation depends on thickness range and width range. The values below reflect the common commercial tables used for 304 cold rolled coil in Asian and European trade; the purchase order should name the standard, not just the numbers.
| Parametru | Common range | Typical tolerance | Inspection method |
|---|---|---|---|
| Grosime, laminate la rece | 0.3 la 3.0 mm | plus sau minus 0.02 la 0.10 mm | Micrometer, 10 mm from edge and at mid width |
| Grosime, laminate la cald | 3.0 la 12.0 mm | plus sau minus 0.15 la 0.45 mm | Micrometer at three points across width |
| Lăţime | 600 la 1500 mm | 0 to plus 5 mm, or minus 0 to plus 3 mm for slit edge | Tape at coil face, three readings |
| Inner diameter | 508 sau 610 mm | plus sau minus 5 mm | Tape across the eye |
| Greutatea bobinei | 2 la 8 t, până la 25 t by agreement | minus 5 to plus 10 percent per coil | Weighbridge ticket per coil |
| Bomba | Measured over 3 m | 5 mm max for cold rolled, 10 mm max for hot rolled | String line on the uncoiled strip |
| Edge burr | Slit edge only | 0.15 mm max, no continuous turn down burr | Visual and fingernail check at four points |
Mill edge coil is coil that has not been side trimmed. Its width carries the hot rolling tolerance and its edge shows a rounded or slightly wavy profile. Slit edge coil has been trimmed by rotary knives, giving a defined width and a straight edge, at the cost of a burr that must be controlled. The choice is not cosmetic: a roll forming line that tracks the edge needs slit edge, while a blanking line that trims the blank afterwards can tolerate mill edge.
5. Coil Geometry: Greutate, Inner Diameter and Outer Diameter
A coil is a spiral of strip, so its weight can be calculated from the strip section and the length. For a coil of thickness t in millimetres, width w in millimetres and density 7.93 g/cm3, one metre of strip weighs 7.93 x t x w / 1000 kilograme. O 1.2 mm x 1219 mm coil therefore weighs 11.6 kg per metre, si a 4 tonne coil contains about 345 metres of strip.
The outer diameter follows from the wound length and the inner diameter. Pentru a 508 mm inner diameter and 4 tonne coil at 1.2 mm, the outer diameter typically lands between 1400 şi 1600 mm. That number matters because it sets the coil’s footprint in a container, the clearance under a crane, and whether the coil fits the decoiler mandrel with the available expansion range.
Heavy coils reduce handling cost per tonne and improve line efficiency, because every coil change costs time. They also raise every downstream requirement: crane capacity, mandrel capacity, floor loading, and the risk of damage if a coil is set down hard. For a buyer with a 5 tonne crane and a light slitting line, o 12 tonne mill coil is not a bargain; it is a handling problem that will be solved by cutting the coil on site at extra cost.
6. Container Loading Arithmetic
Coil shipments are limited by payload and by volume, and the two limits rarely bind at the same time. O 20 foot container is normally loaded to about 21 la 25 tonnes of steel, while a 40 foot container is limited to about 26 la 27 tonnes by road weight rules in many destinations even though the box itself could hold more. Stainless coil at 7.93 g/cm3 is dense, so once the payload limit is reached there is usually space left in the box.
Coils can be loaded eye to sky or eye to side. Eye to sky uses a cradle or a coil stand and keeps the coil upright, which is the safest orientation for the strip because the laps are not bearing on each other, but it consumes height and needs more dunnage. Eye to side, with the coil axis across the container, packs more tonnes per metre but requires wedging and banding so the coil cannot roll, and it loads the coil face against the floor. Pentru 304 with a 2B finish, eye to side loading without interleaving is a common cause of surface scratches discovered at destination.
A practical rule for a 20 foot container of 1.2 mm x 1219 mm 304 coil is four coils of about 5 tonnes each, loaded eye to sky on cradles, giving roughly 20 tonnes net with the coils separated by timber. The same box loaded eye to side can take six coils of 4 tone, but the packing plan must show the wedges and the lashing points, and the buyer should expect more edge deformation on the outer laps.
7. Processing and Manufacturing Points
O 304 coil is only half a product. What happens between the coil and the blank decides whether the material performs as the certificate suggests.
Uncoiling tension. Too much tension stretches the strip and leaves residual stress that shows up as bowing after slitting. Too little tension allows the coil to telescope, and the outer laps then rub against each other. A coil that has been stored eye to sky for months tends to develop a set, and the first two or three metres after the eye often carry a visible crossbow.
Taiere. Rotary slitting introduces a burr on one side and work hardening in a narrow band along the cut. Pentru a 1.0 mm strip, a burr of 0.1 mm is normal; above 0.2 mm the burr will mark the next lap and may propagate a crack during roll forming. Knife clearance set too wide produces a turned edge; too tight produces a heavy burr and rapid knife wear.
Levelling. Cold rolled coil carries coil set and sometimes crossbow. A leveller reduces both, but it also introduces its own residual stress pattern. Sheet cut from a coil that was not levelled will show a gap under a straight edge, and that gap is the reason a laser cut nested part sometimes comes out with one corner lifted.
Interleaving and protection. 2B finish coil is usually interleaved with paper or laminated film and banded at three positions. The interleaving protects the surface against abrasion, not against moisture. A coil that is wetted in transit and then left wrapped in a closed container will develop staining under the paper, and the stain is usually charged to the supplier even though the cause is condensation.
Edge condition and downstream scrap. A slit edge with a burr reduces the usable width by the burr height on each side. On a narrow strip job, that loss is real money: 0.3 mm of burr on both sides of a 300 mm strip is 0.2 percent of the material, but it is also the difference between a part that fits the jig and one that does not.
For buyers who need the coil converted into sheet before use, the relevant product page is the 304 stainless steel sheet 2B finish, which is cut from exactly this coil and inspected on the same tables.
8. Selection and Storage Rules
The following rules are the ones that prevent most coil complaints in practice.
- Write the coil weight range, not a single target. A mill that can only supply 8 la 12 tonne coils should be allowed to say so before the order is placed.
- Specify inner diameter as 508 sau 610 mm and confirm the decoiler mandrel range. O 610 mm eye will not run on a 508 mm mandrel without an adapter.
- State edge condition and, if slit edge, the burr limit and whether the burr side must face a particular direction in the finished part.
- For 2B finish, require interleaving on both faces and specify whether paper or film is acceptable in the destination’s waste rules.
- Store coils eye to sky on a cradle or a timber bed, never directly on concrete, and never on a coil face that will later be a visible surface.
- Keep the storage area dry and ventilated. Stainless does not rust through, but condensation under wrapping produces staining that looks like corrosion and is hard to argue away.
- Rotate stock. A coil that has sat for a year will have a set at the eye, and the first laps will need to be scrapped or re-levelled.
9. Common Misconceptions
Misconception one: 304 coil cannot be magnetic. Recoaptă 304 is weakly magnetic at best, but slitting, levelling and bending transform part of the austenite into strain induced martensite, and that zone responds to a magnet. A magnet sticking to a slit edge is not evidence of the wrong grade.
Misconception two: a heavier coil is always cheaper per tonne. It is cheaper at the mill gate and more expensive at the buyer’s gate if the crane, the mandrel or the floor cannot take it. The correct comparison is delivered cost per finished part, not cost per tonne.
Misconception three: thickness tolerance is symmetric. Many mill tables allow more plus deviation than minus, or the reverse, depending on the thickness band. A buyer who needs a minimum structural thickness must order to a minimum, not to a nominal.
Misconception four: 2B finish means the surface is protected. It means the surface has been rolled, annealed and pickled to a dull, uniform finish. It says nothing about scratch resistance, and a 2B coil handled without interleaving will show handling marks within a week.
Misconception five: coil weight and coil length are the same thing. They are linked by thickness and width. Halving the thickness doubles the length at the same weight, which changes the number of coil changes on the line and the handling cost per tonne.
10. Întrebări frecvente
What is the standard inner diameter of a 304 bobina?
508 mm și 610 mm are the two commercial standards. Some mills also supply 400 mm sau 760 mm eyes for specific lines, but those are exceptions and usually carry a minimum order quantity.
How many tonnes fit in a 20 foot container?
For stainless coil, the practical limit is usually 21 la 25 tonnes net, set by road weight rules rather than by the box. Confirm the destination’s axle limits before fixing the coil count.
Should I buy mill edge or slit edge coil?
Buy slit edge when the line tracks the edge, when width tolerance is tight, or when the edge will be visible. Buy mill edge when you will trim the blank anyway and want the lower price.
Can a 304 coil be supplied with a No.4 finish?
Da. No.4 is produced on a polishing line after cold rolling, and it is normally supplied as coil or as cut sheet. It costs more and is more sensitive to handling, so interleaving is essential.
Why does the first metre of a coil look wavy?
That is coil set plus the memory of the eye bend. It is normal, and it is usually cut off and scrapped, or flattened on a leveller before use.
Are 304 coil need a mill test certificate?
For any food, medical, pressure or export application, Da. The certificate ties the coil to a heat number and gives the chemistry and mechanical results that the design assumes.
11. Next Step
If you are ordering 304 bobina, put thickness, lăţime, starea marginilor, coil weight range, diametrul interior, finish and certificate requirement on the enquiry. Those six lines prevent most of the disputes described above, and they let the mill quote against a real specification instead of a guess.
Related product pages: 304 stainless steel sheet 2B finish, 316L placă din oțel inoxidabil.

