 PROGRESUL
Placa de aluminiu 5052 H32: Minimum Bend Radius, Springback and Forming Practice
AA5052 H32 aluminium plate is the workhorse alloy for parts that must be formed, welded and exposed to moisture without paying for a heat-treatable alloy. Fuel tanks, fitinguri marine, caroserii camioanelor, pressure vessels for water and air, signage frames and architectural panels are all routinely made from it. The practical question for a fabricator is rarely “is 5052 good enough”, but “what bend radius can I actually achieve at this thickness, and how much will the material spring back when I release the press”. This guide answers that question with the numbers that matter on the shop floor.
1. Ce 5052 Aluminium Plate Is and Where It Is Used
5052 is a non-heat-treatable aluminium-magnesium alloy. It cannot be strengthened by solution treatment and ageing, so strength comes from cold work and from the magnesium in solid solution. Plate is supplied in the H32 temper, which means the material has been cold rolled to a controlled amount of reduction and then stabilised, giving a yield strength roughly 30 percent above the annealed O temper with useful elongation retained.
Typical applications include:
- Marine hulls, punțile, superstructures and fittings, where salt water rules out 6061 with copper additions in poorly protected joints.
- Fuel and hydraulic tanks for trucks, gensets and agricultural equipment.
- Pressure vessels and air receivers for moderate pressures and ambient temperatures.
- Road signs, sign frames and architectural fascia, often anodised or painted after forming.
- Appliance and electronic enclosures that need formability plus reasonable strength.
- Automotive panels, brackets and heat shields where a ductile, weldable sheet is preferred to a heat-treated one.
2. Compoziție chimică
The registered composition of 5052 under ASTM B209 and EN 485-2 is shown below. Magnesium is the main alloying element, chromium controls grain structure and suppresses susceptibility to stress corrosion cracking, and the impurity limits are tight because iron and silicon form coarse intermetallic phases that reduce ductility.
| Element | Conţinut (%) | Role |
|---|---|---|
| Mg | 2.2–2,8 | Solid-solution strengthening, weldability balance |
| Cr | 0.15–0,35 | Grain refinement, rezistenta la coroziune |
| Fe | ≤ 0.40 | Impuritate; excess reduces ductility |
| Si | ≤ 0.25 | Impuritate; forms Mg2Si with magnesium |
| Cu | ≤ 0.10 | Impuritate; keep low for marine service |
| Mn | ≤ 0.10 | Minor; disperses iron phases |
| Zn | ≤ 0.10 | Impuritate |
| Al | Echilibru | Matrix |
A point that matters for marine fabricators: 5052 is not immune to seawater simply because it is “marine grade”. It performs well because it resists pitting in chloride environments better than 6061, but it still requires a clean surface, no embedded iron contamination and, in immersed service, a protective coating or an alloy with a higher magnesium content such as 5083.
3. Mechanical Properties of H32 Temper
The table below reflects typical values for plate between 1.5 mm și 6 mm, supplied to ASTM B209 H32. Values are for the longitudinal direction unless stated; transverse ductility is lower and should be used for any bend that runs across the rolling direction.
| Proprietate | H32 typical | O temperament (reference) |
|---|---|---|
| Rezistență la tracțiune | 215–275 MPa | 175–245 MPa |
| Rezistenta la curgere (0.2%) | ≥ 160 MPa | ≥ 65 MPa |
| Elongation in 50 mm | 7–12% | ≥ 18% |
| Duritate | 55–65 HB | 45–55 HB |
| Elastic modulus | 68 GPa | 68 GPa |
| Densitate | 2.68 g/cm3 | 2.68 g/cm3 |
The gap between H32 and O is the reason forming decisions cannot be made from a single datasheet. An H32 sheet at 2 mm needs roughly 30 percent more bending force than the same sheet in O temper, and it will spring back further. If the part is deep drawn or bent to a tight radius, specify O temper and accept the lower strength, or plan an intermediate anneal.
4. Plate Dimensions and Tolerances
| Characteristic | Gamă | Typical tolerance | Nota |
|---|---|---|---|
| Grosime | 0.5–6.0 mm (plate range) | ±0.05 mm below 2 mm; ±0.10 mm above 2 mm | Measured 25 mm from edge |
| Lăţime | 1000–1500 mm | 0 / +3 mm | Marginea tăiată |
| Lungime | 2000–3000 mm | 0 / +5 mm | Squareness ≤ 3 mm/m |
| Planeitatea | – | ≤ 5 mm/m for 2–4 mm | Worse after laser cutting |
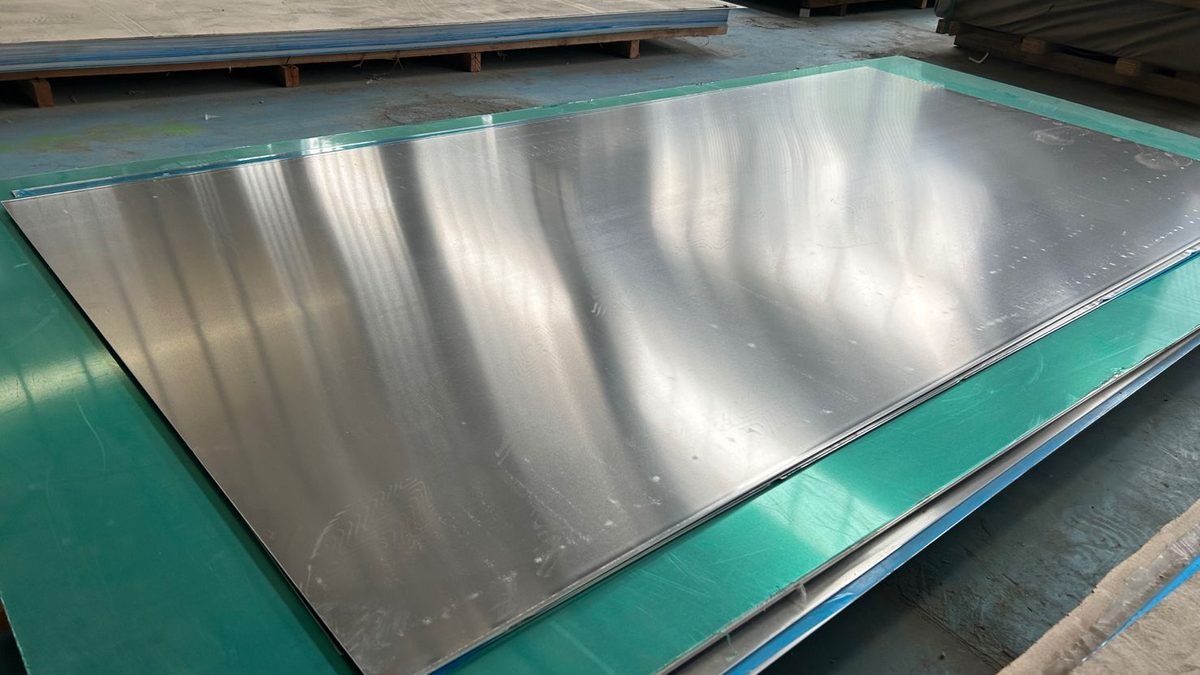
| Suprafaţă | Finisaj moara, Film PVC | No dents, scratches ≤ 0.1 mm deep | Film must be removed before welding |
5. Minimum Bend Radius
Bend radius is normally expressed as a multiple of thickness (t). The values below are practical minimum inside radii for 5052 H32 formed at room temperature with a standard press brake and a punch radius at least equal to the sheet thickness. Going below these figures risks orange peeling on the outside of the bend and cracking at the inside radius.
| Grosime | Bend parallel to rolling direction | Bend across rolling direction |
|---|---|---|
| 1.0 mm | 0.5 t (0.5 mm) | 1.0 t (1.0 mm) |
| 1.5 mm | 0.8 t (1.2 mm) | 1.2 t (1.8 mm) |
| 2.0 mm | 1.0 t (2.0 mm) | 1.5 t (3.0 mm) |
| 3.0 mm | 1.2 t (3.6 mm) | 2.0 t (6.0 mm) |
| 4.0 mm | 1.5 t (6.0 mm) | 2.5 t (10.0 mm) |
| 6.0 mm | 2.0 t (12.0 mm) | 3.0 t (18.0 mm) |
These figures assume the bend line is clean and free of score marks. A scratch 0.1 mm deep on a 2 mm sheet acts as a stress concentration and can halve the achievable radius before cracking starts. Deburring and edge radiusing before bending is not cosmetic; it is what makes the table above achievable.
6. Springback and Bend Allowance
Because 5052 H32 has a high yield strength relative to its modulus, it springs back noticeably. The angle lost after release depends on the ratio of bend radius to thickness and on the die geometry. The table gives typical springback for air bending with a 88-degree die opening.
| Grosime | Inside radius | Springback for 90° bend | Compensation |
|---|---|---|---|
| 1.5 mm | 2 mm | 4°–6° | Over-bend to 94°–96° |
| 2.0 mm | 3 mm | 3°–5° | Over-bend to 93°–95° |
| 3.0 mm | 6 mm | 2°–4° | Over-bend to 92°–94° |
| 4.0 mm | 10 mm | 1.5°–3° | Over-bend to 91.5°–93° |
| 6.0 mm | 18 mm | 1°–2° | Over-bend to 91°–92° |
For bend allowance, use a K-factor of 0.40 la 0.45 for H32 at radius-to-thickness ratios between 1 şi 3, şi 0.45 la 0.50 for ratios above 3. The neutral axis shifts outward as the radius tightens, and a part designed with K = 0.33 will come out short by several millimetres on a 500 mm developed length.
7. Manufacturing and Processing Points
7.1 Rolling and temper
The plate is hot rolled, cold rolled to gauge and then rolled to the H32 reduction. Because the temper is produced by cold work rather than heat treatment, any subsequent thermal operation, including welding and annealing, locally changes the temper. A welded tank therefore has H32 plate away from the weld and O-condition material in the heat-affected zone.
7.2 Tăiere
Laser and waterjet both cut 5052 cleanly up to 6 mm. Plasma cutting leaves a nitride layer on the cut face that must be removed before welding. Shearing is acceptable for straight cuts but produces a slightly work-hardened edge that should be dressed if the part will be bent close to the cut line.
7.3 Formare
Press brake bending is the most common operation. Tooling should be polished and slightly radiused; sharp punch noses mark the inside of the bend and initiate cracks. For roll forming or deep drawing, O temper is preferable, and a liberal coating of drawing lubricant is essential because aluminium galls against steel tooling.
7.4 Sudare
Utilizare 5356 filler for 5052 în majoritatea cazurilor; 5554 is an alternative for higher strength. GTAW with AC and high-frequency start is standard for thin plate, GMAW with pulsed transfer for thicker sections. Two rules dominate quality:
- Remove the oxide layer mechanically or by reverse-polarity cleaning immediately before welding; aluminium oxide melts at over 2000 °C and will not flow with the arc.
- Control heat input. 5052 is not heat-treatable, but excessive heat input coarsens the weld zone and drops joint strength by 20 la 30 la sută.
7.5 Corrosion behaviour and joint design
In clean, dry air, 5052 forms a stable oxide film within minutes and needs no further protection. In coastal air, the same plate develops a grey surface film that is aesthetically poor but structurally harmless. The failure mode that actually matters is crevice corrosion: any joint where water can enter but not drain, such as a plate lapped over a frame without sealant, will pit within a season. Design drainage into the assembly, seal faying surfaces with an appropriate mastic and avoid trapping water behind stiffeners.
Galvanic corrosion is the second risk. Când 5052 is bolted to carbon steel, the aluminium becomes the anode and corrodes around the fastener. Use insulated washers, a dielectric separator between the dissimilar metals and, where possible, stainless or aluminium-alloy fasteners rather than zinc-plated steel. In a marine atmosphere the same rule applies to aluminium-to-stainless contacts, where the aluminium is again the anodic side.
For decorative or long-life exterior work, anodising or a properly applied paint system adds years of service. Both need the same preparation: degresează, remove oxide by mechanical or alkaline treatment, and ensure the surface is free of embedded iron from cutting tools or wire brushes. A single particle of embedded steel will rust and stain the surrounding aluminium within months.
7.6 Incoming inspection before forming
The cheapest place to catch a problem is at goods-in. Four checks cover most of the risk:
- Measure thickness at five points with a calibrated gauge; a plate that is 0.1 mm under gauge will bend differently and will not meet the design weight.
- Check flatness on a surface plate or a straight edge. Residual bow indicates unbalanced rolling and predicts uneven springback.
- Confirm temper with a portable hardness tester or a simple bend trial on a scrap strip; a plate supplied as H32 but actually O temper will fail the yield requirement in service.
- Inspect the surface under oblique light for roll marks, scratches and embedded contamination; these defects become visible only after anodising or painting, when repair is expensive.
8. Selection and Design Rules
- Choose temper by forming severity, not by strength target. Tight radii and deep draws need O temper; flat panels and light bends can use H32.
- Keep bend lines parallel to the rolling direction when the radius is tight. Transverse bends need roughly 50 percent more radius for the same risk of cracking.
- Allow for springback in the tooling or over-bend in the stroke. Do not expect a 90-degree die to produce a 90-degree part on the first trial.
- Specify edge condition and surface protection. PVC film protects during transport but must be removed before any thermal operation.
- For marine or immersed service, specifica 5083 instead of 5052 when the design life exceeds a few years in salt water.
- State the required flatness and the measurement method. Flatness measured on a granite table differs from flatness measured on a pallet.
9. Common Misconceptions
- “5052 is heat treatable, so I can strengthen it after bending.” Nu este tratabil termic. Ageing does nothing, and annealing softens it.
- “H32 and O bend the same; the difference is only yield strength.” Springback, minimum radius and cracking risk all change between tempers.
- “A 1 t radius works for any thickness.” Radius is a multiple of thickness; 1 t on 6 mm plate is a 6 mm radius, which is near the limit and requires polished tooling.
- “Aluminium does not rust, so surface protection is unnecessary.” Aluminium oxidises instantly and the oxide traps moisture and dirt; in chloride service, pitting follows contamination.
- “Any filler wire will do.” 4043 filler on 5052 produces lower ductility and different corrosion behaviour than 5356, especially after anodising.
- “Laser-cut edges are ready to weld.” Laser cutting can leave a thin oxide and a dross edge that must be dressed before a sound weld is possible.
- “Thicker plate is always safer for a tank.” Thicker plate needs larger radii, more force and more heat input, and it does not compensate for a poor joint design.
10. Întrebări frecvente
Can 5052 H32 be bent to a 90-degree angle in one hit?
Yes for thicknesses up to about 3 mm, provided the inside radius is at least 1 t and the bend line runs along the rolling direction. Mai sus 3 mm, bend in two stages or use a larger radius.
Care este diferența dintre 5052 H32 and 5052 H34?
H34 is cold worked to a higher reduction, giving roughly 10 la 15 percent higher yield strength and lower elongation. It springs back more and is less suitable for tight bends.
Does bending across the rolling direction really matter?
It does. Transverse elongation is typically 30 la 40 percent lower than longitudinal, so a bend across the grain needs a larger radius or an annealed temper to avoid cracking.
How much force does a 2 mm 5052 H32 bend need?
Pentru a 1 m wide air bend to a 3 mm inside radius, expect roughly 12 la 18 tonnes on a press brake, depending on die opening. The exact figure depends on the punch and die geometry, so treat this as a starting point for machine selection.
Will anodising change the bend performance?
The anodic layer is brittle. Îndoiți-vă mai întâi, apoi anodiză; bending an anodised part cracks the coating along the bend line and exposes bare metal.
Pot suda 5052 la 6061?
Da, cu 5356 umplutură, but the joint will be limited by the lower-strength alloy and the dissimilar temper behaviour. For structural joints, design the connection so the 6061 side carries less load.
What surface finish should I expect on mill-finish plate?
A uniform rolled finish with occasional roll marks, no deep scratches and no embedded iron. Any dark spots or smears usually indicate rolled-in contamination and should be rejected before forming.
Are 5052 need stress relief after bending?
For most parts, no. For parts that will be machined after forming, or that must hold flatness during anodising, a low-temperature stress relief at 150 la 200 °C for a few hours reduces residual stress without changing temper significantly.
How do I avoid orange peel on a tight bend?
Use a larger punch radius, polish the tooling, keep the bend line parallel to the rolling direction and switch to O temper if the design allows. Orange peel is a surface manifestation of coarse grain, and coarse grain comes from insufficient cold work or excessive annealing.
este 5052 suitable for potable water tanks?
It is used for water tanks, but the alloy is not specified for chlorinated potable water in all jurisdictions. Confirm the local approval, and never use it for acidic or high-chloride water without a lining.
11. Next Step
The safe way to specify 5052 plate is to give the fabricator the finished geometry, not just the alloy: grosime, bend radius, bend direction relative to the rolling direction, temper and surface requirement. Send those details with your quantity and destination, and we will confirm the temper that keeps the part inside the forming limits in the tables above.
Related product pages: 5052 Tabla de aluminiu H32, 6061 Placa din aluminiu T6, 1060 placă de aluminiu pur.

