 PROGRESSO
321 Tubo de Aço Inoxidável: Estabilização, Serviço térmico e soldagem
321 stainless steel tube is the titanium-stabilised version of 18-8 austenitic tube. The titanium addition does not raise room-temperature strength; it prevents chromium carbide from forming at grain boundaries when the tube is held in the 425 para 815 °C band, which is exactly where refinery, petrochemical and exhaust hardware lives. If a drawing calls for 321 and the supplier ships 304, the tube will pass a dimensional inspection and fail in service two or three years later.
O que 321 Tube Is and Where It Is Used
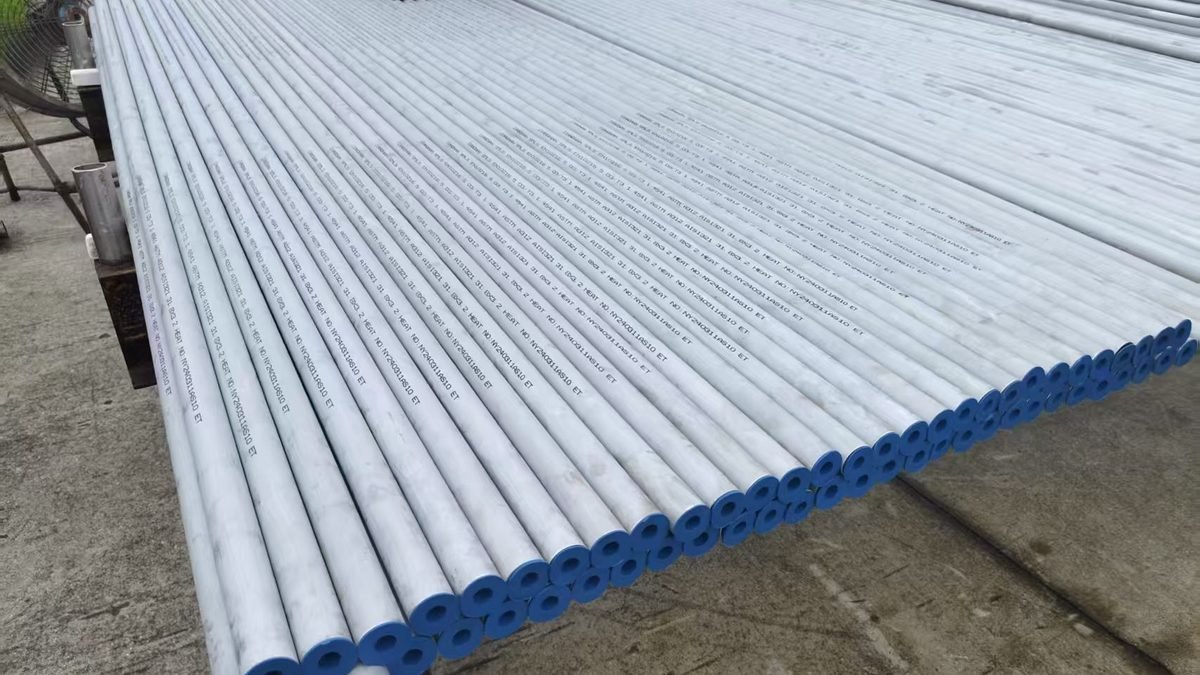
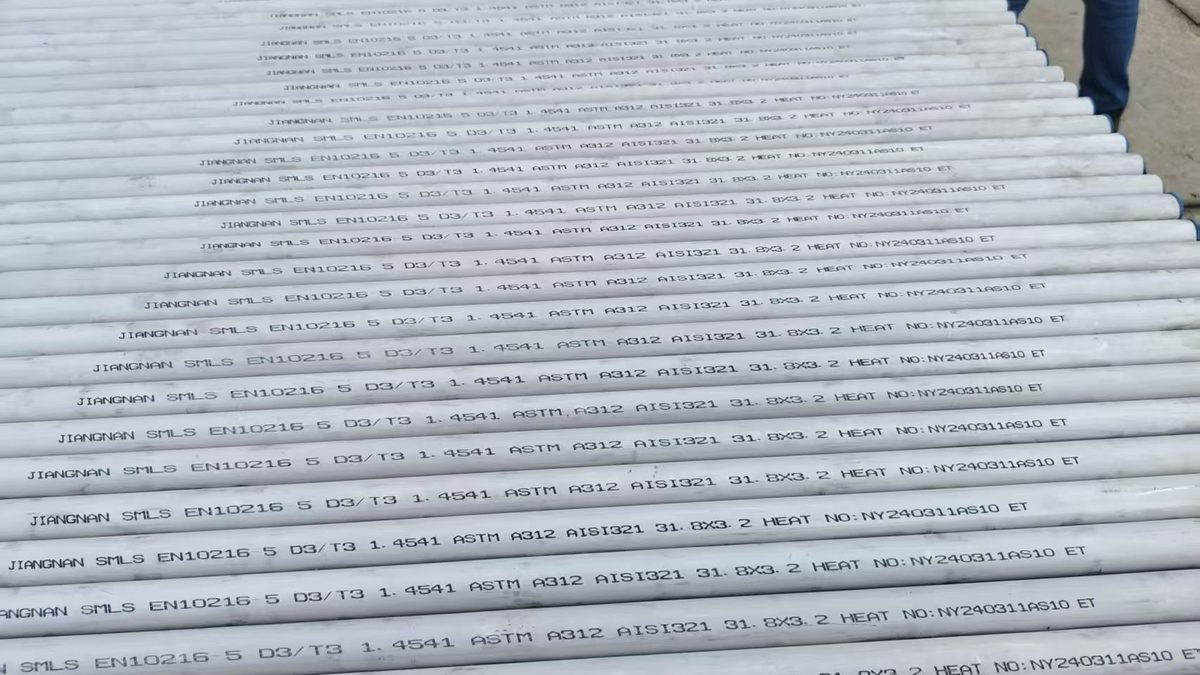
321 is covered by ASTM A312 (welded and seamless austenitic pipe), ASTM A213 (seamless boiler and heat-exchanger tube), ASTM A269 (general seamless tube) e EN 10216-5. The grade designation is TP321 in A312/A213 and 1.4541 in EN, with the UNS number S32100. It is supplied as cold-drawn seamless tube, as welded tube with a longitudinal seam, and as welded-and-drawn tube where the seam is worked and annealed.
The service temperature is the reason to buy it. 321 is used for heat-exchanger tubes in refinery preheat trains, furnace tube supports, catalytic reformer hardware, expansion joints and bellows, exhaust manifolds and downpipes, and high-temperature process piping that sees repeated thermal cycling. It handles continuous service up to about 925 °C in oxidising atmospheres, with lower limits in reducing or sulphidising conditions. In a plain atmospheric application, 304 is cheaper and does the same job.
Grau e composição química
The titanium content is specified as a multiple of carbon, not as a fixed number. ASTM A312 requires titanium of at least five times the carbon content and no more than 0.70 por cento. In practice a mill aims for 0.40 para 0.60 percent titanium so that the ratio stays above five even when carbon sits at the top of its 0.08 percent limit. A heat with 0.03 percent carbon and 0.20 percent titanium would pass a simple chemistry check and still be under-stabilised.
| Elemento | C | E | Mn | P | S | Cr | Em | De | N |
|---|---|---|---|---|---|---|---|---|---|
| Wt. % | 0.08 máx. | 0.75 máx. | 2.00 máx. | 0.045 máx. | 0.030 máx. | 17.0-19.0 | 9.0-12.0 | 5×C min, 0.70 máx. | 0.10 máx. |
ASTM A312 / A213 limits for TP321. Titanium is reported as a range in the mill certificate and the Ti/C ratio should be shown explicitly.
Propriedades mecânicas
The room-temperature minimums are modest and are not the reason anyone specifies 321. What matters is the elevated-temperature rupture strength and the stability of the microstructure after long exposure. The table gives the standard room-temperature values plus the creep-rupture figures that a heat-exchanger design normally uses.
| Propriedade | Valor | Basis |
|---|---|---|
| Resistência à tracção | 515 MPa min | ASTM A312 |
| Força de rendimento, 0.2% | 205 MPa min | ASTM A312 |
| Alongamento em 50 milímetros | 35% min | ASTM A312 |
| Dureza | 90 HRB máx. | ASTM A312 |
| Densidade | 7.92 g/cm³ | Nominal |
| Expansão térmica | 17.3 × 10⁻⁶ /K | 20-800 °C average |
| Condutividade térmica | 16-20 S/m·K | No 500 °C |
| Creep rupture, 1,000 h | Sobre 45 MPa at 800 °C | Design data, verify |
| Max continuous service | 925 °C oxidising | Grade data |
Design values for elevated temperature must come from the applicable code (ASME BPVC Section VIII Div. 1 ou EN 13445), not from a supplier data sheet.
Dimensões e Tolerâncias
Tube is ordered by outside diameter, espessura da parede, length and manufacturing route. Seamless cold-drawn tube holds a tighter concentricity and a better bore finish; welded tube is cheaper above about 219 mm OD and is acceptable where the seam is not in a high-cycle thermal zone. The tolerances below follow the common ASTM and EN practice for each route.
| Parâmetro | Seamless cold drawn | Soldado | Observação |
|---|---|---|---|
| OD range | 6-610 milímetros | 12-1,200 milímetros | Larger on request |
| Wall range | 0.5-30 milímetros | 0.8-20 milímetros | Schedule or metric |
| OD tolerance | ±0.4% or ±0.4 mm | ±0.5% or ±0.5 mm | Whichever is greater |
| Wall tolerance | ±10% | ±10% | Min wall governs design |
| Concentricidade | ≤ 0.10 × wall | ≤ 0.15 × wall | Measured at mid-length |
| Comprimento | Fixed ±3 mm | Fixed ±5 mm | Random 5-7 eu |
| Retidão | ≤ 1 mm por metro | ≤ 1.5 mm por metro | Over full length |
| Bore finish | Ra ≤ 1.6 µm | Ra ≤ 3.2 µm | Pickled or bright annealed |
Tolerances are commercial ranges; the purchase order must name the standard because ASTM A312 and EN 10216-5 limits differ.
How the Tube Is Made
Seamless route
A pierced billet is extruded or a hollow is drilled, then cold pilgered or cold drawn over a mandrel through a sequence of decreasing diameters, with anneals between passes. Each cold reduction adds strength and hardness, so the tube must be solution annealed before delivery. The final anneal is 1,040 para 1,120 °C followed by a fast water quench, which dissolves carbides and puts the titanium back into solid solution where it can do its job.
Welded route
Strip is roll-formed into a cylinder and welded longitudinally, usually by TIG or plasma with 321 ou 347 enchimento. The weld bead is scarfed on the outside and, for hygienic or high-cycle work, on the inside as well. Welded tube is then solution annealed in line or in a batch furnace. If the tube is welded and drawn, the seam is reduced and annealed with the rest of the wall, which improves grain structure and concentricity but adds cost.
Decapagem, passivation and testing
Depois de recozimento, the tube carries a dark oxide scale. It is pickled in a nitric-hydrofluoric bath or a paste, rinsed, and passivated in nitric acid. Over-pickling attacks grain boundaries and leaves a rough bore; under-pickling leaves oxide that spalls into the process fluid. Each lot is hydrotested, eddy-current or ultrasonic tested, and a flattening or flaring test is done on samples. Intergranular corrosion resistance is checked by ASTM A262 Practice E on a sensitised specimen for critical service.
Welding and High-Temperature Rules
Use an 18-8 Nb filler such as ER347 for welding 321 to itself or to 304. Niobium and titanium both stabilise carbon, and the weld metal needs its own stabiliser because the titanium in the parent metal does not fully transfer across the arc. Do not use 308L filler on a 321 heat-exchanger tube: the weld becomes the sensitised zone that the grade was selected to avoid.
Thin-wall tube up to about 3 mm usually needs no post-weld heat treatment if the heat input is controlled and the joint is not in a high-cycle thermal zone. Acima disso, or where the weld will operate in the 425 para 815 °C band, a stabilising anneal at 870 para 900 °C for one hour per 25 mm of thickness, followed by air cooling, is the standard treatment. A full solution anneal at 1,040 para 1,120 °C is better metallurgically but causes more distortion and scale on finished tube.
Design for thermal movement. A 6 metre tube that goes from ambient to 800 °C grows about 80 milímetros. If both ends are rigidly anchored, the expansion becomes compressive stress and the tube bows or cracks at the support. Leave expansion loops, sliding supports or bellows at the correct spacing, and do not use the tube as a structural strut in a hot line.
321 Against 304, 316Terra 347
The four grades overlap enough to confuse a buyer, so compare them on the variable that matters. 304 has the same 18-8 base without titanium; it is cheaper and perfectly adequate below 400 °C, but after long exposure in the 425 para 815 °C band its grain boundaries become chromium-depleted and the tube is sensitised. 321 adds titanium and holds its intergranular corrosion resistance through that band, which is the whole point of the grade.
316L adiciona 2.0 para 3.0 percent molybdenum, which buys resistance to chlorides and to reducing acids, but it is not stabilised against sensitisation in the same way and its allowable stress at 600 °C is lower than that of 321. A heat exchanger that sees both chlorides and 600 °C is a genuine materials-engineering problem, and the usual answer is a higher-alloy grade rather than either 316L or 321 sozinho.
347 is the niobium-stabilised sibling. Niobium is less mobile than titanium during welding and does not oxidise away at the arc, so heavy-section welds retain their stabilisation more reliably. For seamless tube the difference rarely shows; for welded tube with a thick seam, 347 é a escolha mais segura. European drawings often call 1.4541 where American drawings call TP321, and they are the same grade.
| Nota | Stabiliser | Resistência ao cloreto | Hot-band stability | Uso típico |
|---|---|---|---|---|
| 304 / 1.4301 | Nenhum | Moderado | Poor above 425 °C | General ambient service |
| 321 / 1.4541 | Ti ≥ 5×C | Moderado | Bom | Trocadores de calor, furnace parts |
| 316eu / 1.4404 | Nenhum | Bom | Moderado | Chemical, marinho, pulp |
| 347 / 1.4550 | N.º + Ta | Moderado | Bom | Heavy welded hot sections |
Guide only; final selection must consider the actual atmosphere, chloride level, cycle frequency and code allowable stress.
Specifying a Heat-Exchanger Tube
A heat-exchanger tube order needs more than a diameter and a wall. Start with the standard: ASTM A213 covers seamless ferritic and austenitic boiler and heat-exchanger tube, while A312 covers both welded and seamless pipe for high-temperature service. They differ in test schedule, tolerance and marking, and a supplier who quotes “ASTM A312/A213” without saying which one governs is leaving the acceptance criteria open.
Próximo, state the wall basis. Tube is bought on average wall or minimum wall, and the two are not interchangeable. A 2.77 mm average wall tube can have 2.49 mm at one point and still pass; a 2.77 mm minimum wall tube cannot. For a pressure-retaining bundle, design on minimum wall and say so on the order. Then add the tests: hydrostatic or pneumatic, eddy-current, ultrasonic, achatamento, flaring, and the intergranular corrosion test if the service is wet and hot.
Finalmente, specify the delivery condition and the bore. Solution annealed, pickled and passivated is the normal condition. Bright annealed tube is available for clean service but costs more. State whether the bore must be free of scale, whether a plug or cap is required, and how the ends are protected in transit. A bundle of pickled tube shipped in a damp container will arrive with rust stains that no amount of re-passivation will fully remove.
Corrosão, Cleaning and Storage
321 resists oxidising acids and most process streams but is not immune to chloride pitting, crevice attack or stress-corrosion cracking. The titanium stabilisation protects grain boundaries; it does nothing for a chloride ion sitting in a crevice under a baffle. Keep chloride levels in the cooling water within the design limit, avoid stagnant low-flow conditions, and do not use chloride-bearing cleaning chemicals on a freshly pickled bundle.
Cleaning should be mechanical plus a nitric passivation, not a hydrochloric acid descaler. Hydrochloric acid will pit the tube and leave it worse than before. For organic fouling, a mild alkaline wash followed by a thorough rinse is enough; for scale, a chelating or nitric-based product matched to the alloy is the safe route. After any wet cleaning, dry the bundle with oil-free air before it goes back into service.
Storage follows the same logic. Keep tube off the ground, sob cobertura, with the ends capped or taped, and do not stack bundles so that water sits in the low tube. If the tube is stored for more than a few months in a humid climate, re-check the bore for staining before fabrication. A stain that is only cosmetic can be removed; a pit that has started cannot.
Regras de Seleção
- Specify TP321 or 1.4541 with the Ti/C ratio on the certificate, não apenas “321”.
- State the standard (ASTM A312, A213, A269 or EN 10216-5); the tolerances and test schedule differ.
- For heat-exchanger service, specify seamless cold-drawn tube and the eddy-current test.
- For welded tube, state whether the inside bead must be scarfed and whether the seam may sit in the hot zone.
- State the heat treatment condition: solution annealed, pickled and passivated.
- For critical wet service, add ASTM A262 Practice E and a ferrite check if the spec requires it.
- Do not substitute 304 or 316L without a written engineering review; the substitution changes the elevated-temperature life.
Erros Comuns
- Accepting a certificate that lists titanium without the carbon content, so the Ti/C ratio cannot be checked.
- Buying 321 for chloride service. Titanium stabilisation does nothing for pitting in seawater; use 316L, 904L or a duplex grade.
- Welding with 308L filler because it was in the store. The weld becomes the weak link in the hot zone.
- Over-pickling the bore to make it look bright, then finding intergranular attack at the first hydrotest.
- Using welded tube with an unscarfed inside bead in a heat-exchanger bundle; the bead collects fouling and erodes.
- Supondo 321 is stronger than 304 at room temperature. The minimums are essentially the same.
- Anchoring both ends of a hot tube run and blaming the tube when it bows.
- Storing pickled tube with wet rags between bundles; the passivation is destroyed by trapped moisture.
Perguntas frequentes
É 321 better than 304 for high temperature?
Sim, in the 425 para 815 °C band. The titanium prevents chromium carbide precipitation at grain boundaries, so the tube resists intergranular corrosion after long exposure. Abaixo 400 °C the two grades behave almost identically and 304 is cheaper.
Qual é a diferença entre 321 e 347?
347 uses niobium instead of titanium for stabilisation. Both resist sensitisation; 347 is preferred for welded heavy sections because niobium is less prone to loss during welding, enquanto 321 is common in seamless tube and European specifications.
Pode 321 tube be used in seawater?
Não. It is an unstabilised-chloride-sensitive austenitic grade with no molybdenum. Seawater service needs 316L at minimum, and usually a higher-alloy or duplex grade for flowing or crevice conditions.
Faz 321 need post-weld heat treatment?
For thin-wall, low-cycle work, usually not. For thickness above 3 mm or service in the sensitisation band, a stabilising anneal at 870 para 900 °C is specified. A full solution anneal is used when maximum corrosion resistance is required.
How do I check the Ti/C ratio?
Ask for carbon and titanium on the mill certificate, then divide Ti by C. It must be at least 5. Some mills report the ratio directly; if they do not, do the arithmetic before releasing the heat.
What is the maximum service temperature?
Sobre 925 °C continuous in clean oxidising air, less in reducing or sulphidising gases, and much less when the tube carries pressure. Use the code allowable stress at temperature rather than a single headline number.
For the flat-product side of the stainless range, see the 316L stainless steel plate page or the 304 2B cold-rolled sheet page. Tube enquiries are quoted against OD, parede, padrão, length and test schedule.
Send Your 321 Tube Requirement
DE, parede, comprimento, standard and test schedule are the four lines we need.

