 הִתקַדְמוּת
PVD-Coated Perforated Stainless Steel Facade Panels: Open Area, Film and Fixing
A PVD-coated perforated stainless steel facade panel combines three things that are usually specified separately: a perforated 304 sheet that controls light, air and visual depth; a thin vacuum-deposited ceramic film that gives the surface its gold, champagne or black colour; and a fixing system that holds the panel flat and lets it move with temperature. Each of the three can fail on its own, and each has its own tolerance. This guide explains how the open area is calculated, what a PVD film actually is, which panel sizes and flatness values are realistic, and how the panels should be fixed so that the coating survives.
What the Panel Is and Where It Is Used
The base is a cold-rolled 304 יריעת אל חלד, perforated with round, square or slotted holes on a regular pitch, then cut to panel size, flattened and coated. The coating is applied by physical vapour deposition: the panel is placed in a vacuum chamber, the coating metal is vaporised, and the vapour condenses onto the surface as a thin, hard film. Because the process is line-of-sight, the panel is usually coated flat, before any folding, and the coated face is protected through fabrication and transport.
The product is used where a metal facade needs to look like something other than plain stainless: entrance canopies, screen walls, balcony balustrades, ventilated facade layers, atrium linings, lift lobby feature walls, and shopfront surrounds. In each case the perforation does the visual work — depth, shadow, transparency — and the coating does the colour work.
The distinction from a painted panel is worth stating plainly. Paint is a polymer film 20–60 µm thick that sits on the surface; a PVD film is a ceramic or nitride layer 0.2–2 µm thick that is bonded to the metal and is harder than the substrate. Paint can be repaired with a touch-up pen; PVD cannot, because the colour is created by optical interference in a film that a brush cannot reproduce. That single difference drives most of the handling and fixing rules in this guide.
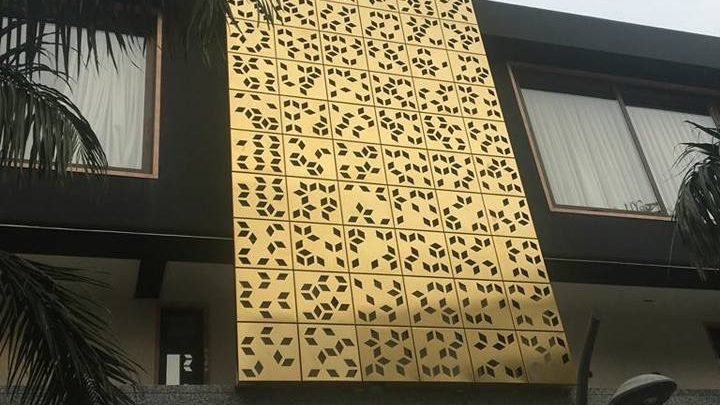
Base Metal and Film Chemistry
צִיוּן 304 is the normal substrate. It provides the corrosion resistance, the stiffness and the flatness that the facade needs, and it accepts the PVD pre-treatment without difficulty. The film itself is one of a small family of hard coatings, each of which produces a different colour because of its refractive index and thickness.
| שִׁכבָה | Nominal thickness | Colour | קַשִׁיוּת (HV) | Notes |
|---|---|---|---|---|
| TiN | 0.5 – 1.5 מיקרומטר | זָהָב | 2 000 – 2 400 | The classic gold; colour shifts with thickness |
| ZrN | 0.5 – 1.5 מיקרומטר | Champagne / pale gold | 2 200 – 2 600 | Brighter, less red than TiN |
| TiCN | 1 – 3 מיקרומטר | Grey-brown to black | 2 800 – 3 200 | Hardest of the common films |
| CrN | 1 – 3 מיקרומטר | Dark grey / שָׁחוֹר | 1 800 – 2 200 | Good wear resistance, neutral colour |
| TiAlN | 1 – 3 מיקרומטר | Anthracite / bronze-black | 2 600 – 3 000 | Used for dark architectural tones |
Indicative film data; the coater’s process specification governs thickness and colour tolerance.
Base metal composition is the same 304 window as any other stainless sheet: C ≤ 0.08, Cr 18.0–20.0, Ni 8.0–10.5, Mn ≤ 2.00, Si ≤ 1.00, P ≤ 0.045, S ≤ 0.030. Two points matter more for PVD than for plain sheet. רֵאשִׁית, surface defects are amplified: a scratch or an inclusion that is invisible on 2B sheet becomes a visible line under a gold film, because the film follows the topography and the colour changes with the local angle. שְׁנִיָה, the substrate must be clean and oxide-free before coating, so the sheet is normally polished or brushed, then chemically cleaned and plasma-etched in the chamber. A mill surface with residual oil will produce a cloudy film that fails the colour match.
Colour consistency is the hardest specification to write. A PVD colour depends on film thickness to within tens of nanometres, so two panels coated in different batches can differ visibly when they are installed side by side. The practical answer is to coat a whole facade in one batch, or to specify a colour difference tolerance (ΔE ≤ 1.5 אֶל 2.0) measured on a spectrophotometer against a master sample, and to keep the master sample available for site comparison.
Mechanical Properties of the Coated Sheet
The PVD film adds hardness, not strength. The panel’s structural behaviour is that of the 304 דַף, thinned by the perforation. This is the number that designers underestimate: א 2 mm sheet with 40 % open area behaves, in bending, like a much thinner continuous sheet, and its deflection under wind load is several times that of the solid panel.
| נֶכֶס | 304 דַף, חישול | Perforated panel, 40 % open area | Comment |
|---|---|---|---|
| חוזק מתיחה | 515 – 700 MPa | Approximately 70 – 80 % of solid | Net section governs |
| 0.2 % proof stress | ≥ 205 MPa | Net section governs | Hole pattern creates stress concentration |
| הַאֲרָכָה | ≥ 40 % | Reduced at hole edges | Hole edge is the crack initiation site |
| Bending stiffness | הַפנָיָה | Roughly 40 – 60 % of solid | Falls faster than strength |
| Surface hardness | ≈ 200 HV | 2 000 – 3 000 HV at the film | Film resists scratching, not denting |
| Film adhesion | — | Typically > 5 N/cm² in scratch test | Coater’s test report required |
Indicative values for 2 מ"מ 304 with a regular round-hole pattern; the actual net-section properties depend on pattern geometry.
The film’s hardness is often quoted as a selling point, and it is real: a TiN film at 2 200 HV will resist keys and cleaning pads far better than bare stainless. But hardness is not toughness. A point load that dents the panel will crack the film at the dent, and the crack shows as a dark line because the exposed substrate reflects differently. A perforated panel is more dent-prone than a solid one, so the film’s hardness does not make the panel robust — it only makes the surface scratch-resistant.
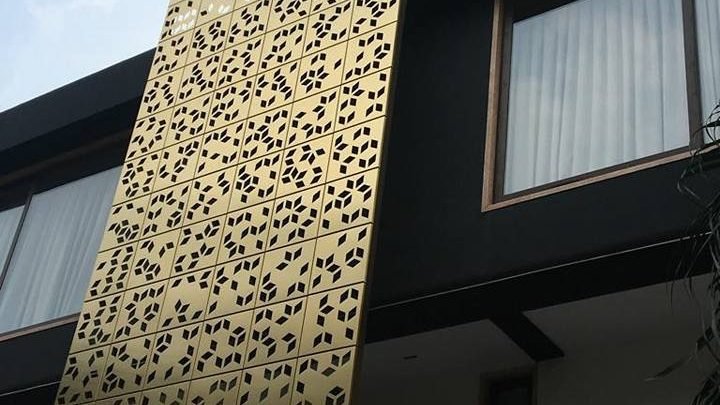
Perforation: Open Area and Pattern
Open area is the percentage of the panel surface that is hole. It is calculated from the hole size and the pitch, and it is the parameter that decides both the visual transparency and the ventilation.
For round holes on a square pitch: open area = (π/4) × (d / p)² × 100 %, where d is the hole diameter and p is the pitch. For a 6 mm hole on a 12 mm pitch, the open area is about 19.6 %. For a 8 mm hole on a 10 mm pitch, it is about 50 %. Staggered patterns give a slightly higher open area for the same pitch, and slot patterns are calculated by the slot area rather than the circle.
| Hole diameter (מ"מ) | Pitch (מ"מ) | תַבְנִית | Open area (%) | Visual effect |
|---|---|---|---|---|
| 3 | 6 | מְרוּבָּע | 19.6 | Fine screen, reads as a solid surface at distance |
| 5 | 10 | מְרוּבָּע | 19.6 | Standard screen; good balance of depth and transparency |
| 6 | 12 | Staggered | 22.7 | Softer image; less moiré against other grids |
| 8 | 10 | מְרוּבָּע | 50.3 | Open, ventilated; substrate visible behind |
| 10 | 12 | Staggered | 63.0 | Very open; needs a backing or a strong subframe |
Calculated open area for round holes; slot and square-hole patterns require their own calculation.
Moiré is the practical problem with fine perforation. A regular hole grid superimposed on another regular grid — a distant railing, a brick facade, a camera sensor — produces a visible interference pattern that shimmers as the viewer moves. A staggered pattern reduces it, and a slightly irregular or graduated pattern removes it, at the cost of a more complex punching programme.
Panel Size, Thickness and Tolerance
Panel size is limited by three things: the coater’s vacuum chamber, the flatness that can be held after perforation, and the wind load. Most architectural PVD lines can coat panels up to about 1 500 × 3 000 מ"מ; beyond that the panel is coated in sections and the colour match risk rises.
| פָּרָמֶטֶר | Typical value or tolerance | Comment |
|---|---|---|
| עוֹבִי | 1.0 – 3.0 מ"מ; tolerance per EN 10088-2 | 2 mm is the common architectural choice |
| Panel size | עד 1 500 × 3 000 מ"מ | Confirm the coater’s chamber before design |
| Hole diameter | ± 0.1 mm for ≤ 6 מ"מ; ± 0.2 mm above | Laser or CNC punch; punch tool wear matters |
| Hole position | ± 0.3 mm within a panel | Cumulative pitch error must be controlled |
| שְׁטִיחוּת | ≤ 1.5 mm/m, ≤ 3 mm overall | Measured on a surface table, coated face up |
| Squareness | ≤ 1 mm per 1 000 מ"מ | Diagonal measurement |
| Colour | ΔE ≤ 1.5 – 2.0 against master | Spectrophotometer, same light source |
| Film thickness | As specified ± 20 % | Coater’s coupon test |
Indicative architectural tolerances; project specification and coater capability govern.
Flatness is where perforated panels differ most from solid ones. Perforation releases the internal stress of the coil, and the panel can bow by several millimetres after punching. Flattening after perforation, and coating the panel flat rather than after folding, are the two measures that hold the tolerance. A panel that is folded before coating will have a film that is thinner on the bend and may crack at the fold line.
Fabrication and Fixing
The sequence for a facade panel is: perforate, flatten, לחתוך לגודל, fold or form the edges, then coat. Folding before coating is acceptable only if the fold is gentle and the coater can reach the folded face; most architectural work coats flat panels and uses a separate edge trim or a folded return that is coated on one side only.
- Perforate by laser or CNC punch; laser leaves a slight taper and a dark edge, which is visible on a gold panel unless it is dressed.
- Deburr both faces; a burr on the coated face will show as a bright ring after coating and as a scratch risk during handling.
- Flatten between rollers or in a press after perforation, and check flatness before coating, because coating locks the shape in.
- Coat flat, with the visible face up; mask the areas that will be welded or fixed with clips if they must remain uncoated.
- Handle coated panels with clean gloves and interleaved paper; a fingerprint on a PVD film etches into the surface within days.
Fixing follows the same logic as any ventilated facade: a subframe of aluminium or galvanised steel, a clip or a bracket that holds the panel at its edges, and a joint wide enough to let the panel move. The panel must not be fixed through the coated face with a self-tapping screw, because the screw head crushes the film and the repair is impossible.
- Use a subframe that is set out to the panel module, not to the structural frame, so the joints stay parallel.
- Fix with edge clips or a concealed bracket; keep the coated face free of fasteners.
- Leave a joint of 8–12 mm between panels for thermal movement and tolerance; a tight joint will close and crush the edges.
- Isolate stainless from aluminium or carbon steel with a gasket or a coating; a direct couple stains the stainless at the contact.
- Do not seal the ventilated cavity with a continuous gasket; the system needs an air path to dry the cavity.
- Clean with a neutral detergent and a soft cloth; acid or abrasive cleaners attack both the film and the substrate.
Wind Load, Cavity and Drainage
A perforated panel is not a sealed cladding. Wind passes through the holes and loads the layer behind it, while the panel itself sees a reduced pressure difference across its face but a much higher local load at the hole edges. The design consequence is that the subframe, not the panel, carries the wind: the rail spacing must be set from the panel’s reduced stiffness and from the suction pressure on the cavity, and the panel is treated as a skin that transfers load to the rails at its edges.
The cavity behind the panel must be ventilated and drained. A perforated screen that is sealed at its base becomes a trap for rain and condensate; the water sits against the substrate, and the staining shows through the holes as dark streaks within a season. Provide an open joint at the bottom of each panel module, a drained cavity membrane behind, and a continuous air path from bottom to top. Do not fill the cavity with insulation that touches the back of the panel, because the insulation stays wet.
Movement joints follow the same rule as the panel joints. א 1 200 mm panel of 304 at a 40 °C surface swing moves about 1.3 מ"מ, and the joint must absorb that plus the fabrication tolerance of both panels and the subframe. An 8 mm joint is the practical minimum for architectural work, and 10–12 mm is safer on dark colours, where a closed joint is more visible.
Common Mistakes
- Specifying a colour by name only. Gold is not a colour number; two suppliers will produce two golds. Specify ΔE against a master sample.
- Ignoring the loss of stiffness from perforation. א 40 % open panel deflects far more than the solid sheet the designer modelled.
- Coating after folding. The film thins and cracks at the bend, and the crack is a corrosion site.
- Fixing through the coated face. The fastener crushes the film irreparably; use clips or concealed brackets.
- Using a tight panel joint. Thermal movement closes the joint, the edges touch, and the coating chips at the contact.
- Cleaning with acid or scouring powder. Both attack the film and leave a permanent dull patch.
שאלות נפוצות
How thick is the PVD coating?
Typically 0.5–1.5 µm for gold TiN and 1–3 µm for dark TiCN or CrN films. It is a fraction of a human hair, but hard enough to resist normal cleaning and light scratching.
Can a scratched PVD panel be repaired?
לֹא, not invisibly. The colour comes from optical interference in a film that cannot be reproduced by a brush or pen. A scratched panel is normally replaced, or the scratch is accepted if it is outside the visible zone.
Does PVD coating affect corrosion resistance?
The film is dense and adherent, so it improves wear resistance and adds a barrier, but it is thin and can be breached at cut edges and scratches. The corrosion resistance still depends on the 304 substrate, so coastal projects should use 316L base metal.
What open area should a facade panel have?
Between about 20 % ו 50 % for most architectural screens. Below 20 % the panel reads as a solid surface; above 50 % the substrate behind becomes dominant and the panel needs more subframe support.
Why do two panels look different in colour?
They were coated in different batches, or the film thickness differs by tens of nanometres. Specify a ΔE tolerance against a master sample and coat one facade in one batch.
How should PVD panels be cleaned?
Neutral pH detergent, soft cloth or sponge, and a rinse with clean water. Avoid acid, alkaline concentrates, scouring pads and anything containing chloride.
Planning a PVD perforated stainless facade?
Send the panel size, hole pattern, open area, colour target and fixing detail; we will confirm coating capacity and tolerance.
Base sheet for the same project: 304 2B cold-rolled stainless sheet, ו 316צלחת L for coastal or chloride-bearing sites.

